OUR MANUFACTURING CAPABILITIES
Advanced ultrasonic plastic welding and thermal fusion joining providing clean, high-strength, hermetically sealed joints without fasteners, solvents, or adhesives.
IATF 16949
Quality standard
Automotive
& appliance grade
Turnkey
Engineering support
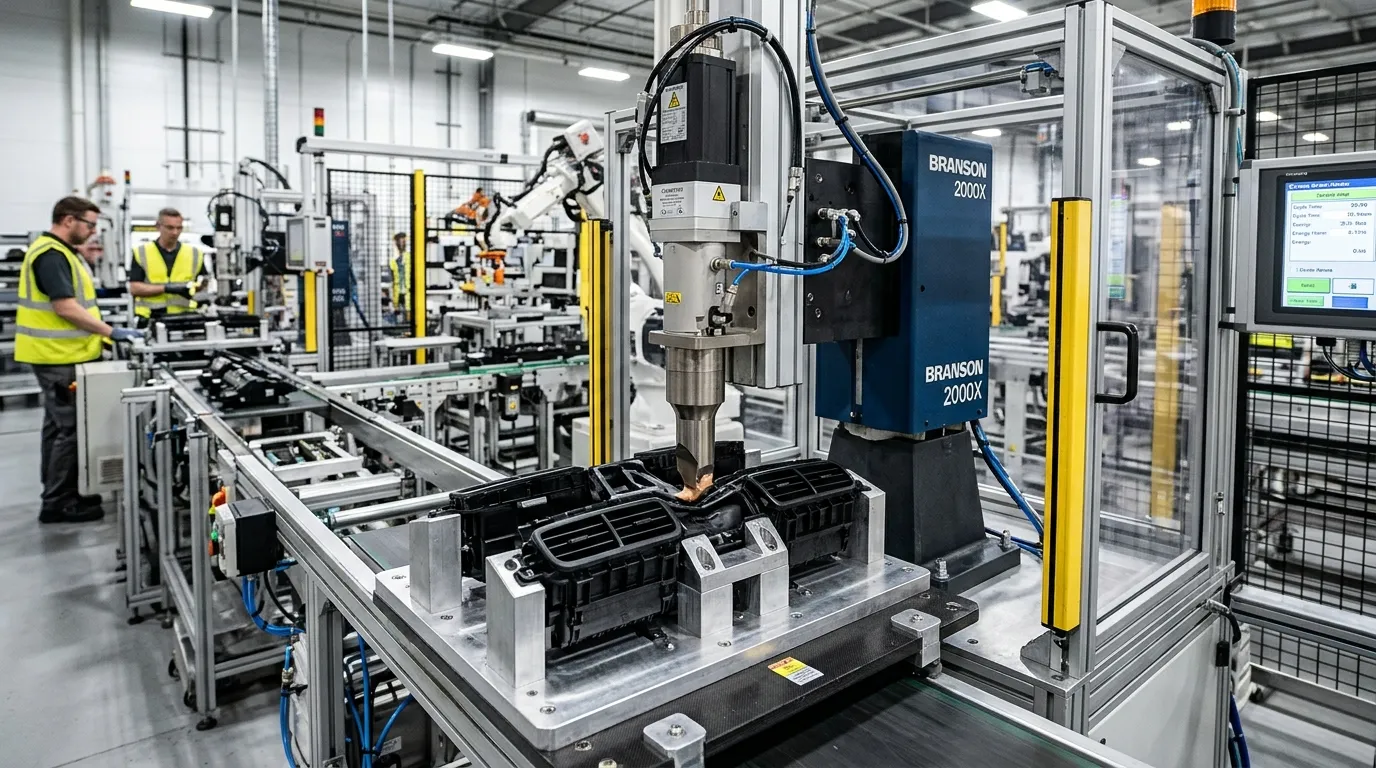
Joining two or more moulded plastic halves into a unified, leak-proof assembly requires precise energy delivery and controlled joint design. We deploy both ultrasonic welding and thermal fusion technologies depending on component geometry, polymer compatibility, and structural demands.
Ultrasonic welding utilizes high-frequency acoustic vibrations (typically 20 kHz to 35 kHz) applied under pressure to create localized frictional heat at joint energy directors, producing molecular fusion in fractions of a second. For larger parting lines or thicker-wall parts, thermal fusion provides robust, continuous, high-integrity welds.
Distinguishing ultrasonic acoustic welding and thermal fusion joining for optimum application matching.
Ideal for rigid amorphous and semi-crystalline polymers (ABS, PC, SAN, Acrylic). Delivers rapid, aesthetically clean joints with minimal thermal stress.
Employed for broad-tolerance or polyolefin components (PP, PE) using controlled hot platen heating to form deeply fused, continuous structural seams.
Custom titanium and aluminium sonotrodes (horns) engineered to resonate uniformly, supported by contour-matched rigid polyurethane/aluminium nests.
Modern computerized welding controllers terminate cycles precisely upon reaching programmed collapse depth or total Joules of energy.
Standardized stages ensuring structural joint strength and cosmetic perfection.
The lower moulded component is positioned securely into an anodized aluminium fixture contoured to absorb welding reaction forces.
Control focusVibration Dampening
The upper component is seated, with moulded energy directors (triangular ridges) or shear joints resting in positive alignment.
Control focusEnergy Director Contact
The weld horn descends under regulated pneumatic force; once trigger force is confirmed, ultrasonic vibrations commence instantly.
Control focusTrigger Force Threshold
Friction melts the energy director, allowing parts to collapse to the programmed depth before holding pressure solidifies the molten joint.
Control focusHold Solidification
Welded assemblies undergo visual flash inspection and, where required, pneumatic decay leak testing or burst pressure checks.
Control focusJoint Integrity Check
Because welded seams often contain fluids or support mechanical loads, our quality procedures verify joint strength and sealing reliability.
Components requiring fluid or air tightness are pressurized to verify that leak decay rates stay well below customer-specified limits.
Pressure Decay Verified
Periodic destructive sampling pulls welded halves apart to confirm cohesive failure within the base polymer rather than along the weld interface.
Cohesive Bond Strength
Moulded flash traps are inspected to confirm that displaced molten plastic is neatly contained without external burrs.
Clean Parting Lines
Height gauges verify that total assembled component height post-welding remains within strict assembly tolerances.
Height Stack-Up
Applied where components cannot be moulded in a single piece due to internal hollows or undercut geometry.
Automotive Components
HVAC air distribution ducting, fluid reservoir tanks, tail lamp housings, and exterior mirror shell assemblies.
Typical components
Home Appliances
Washing machine detergent dispenser bodies, water softener valve chambers, steam iron water tanks, and float valves.
Typical components
Electrical Enclosures
Tamper-evident smart electricity meter casings, electronic timer housings, and sealed wireless sensor pods.
Typical components
What we do
Turnkey component integration, clip insertion, mechanical fastening, and functional testing delivering line-ready sub-assemblies directly to customer production tracks.
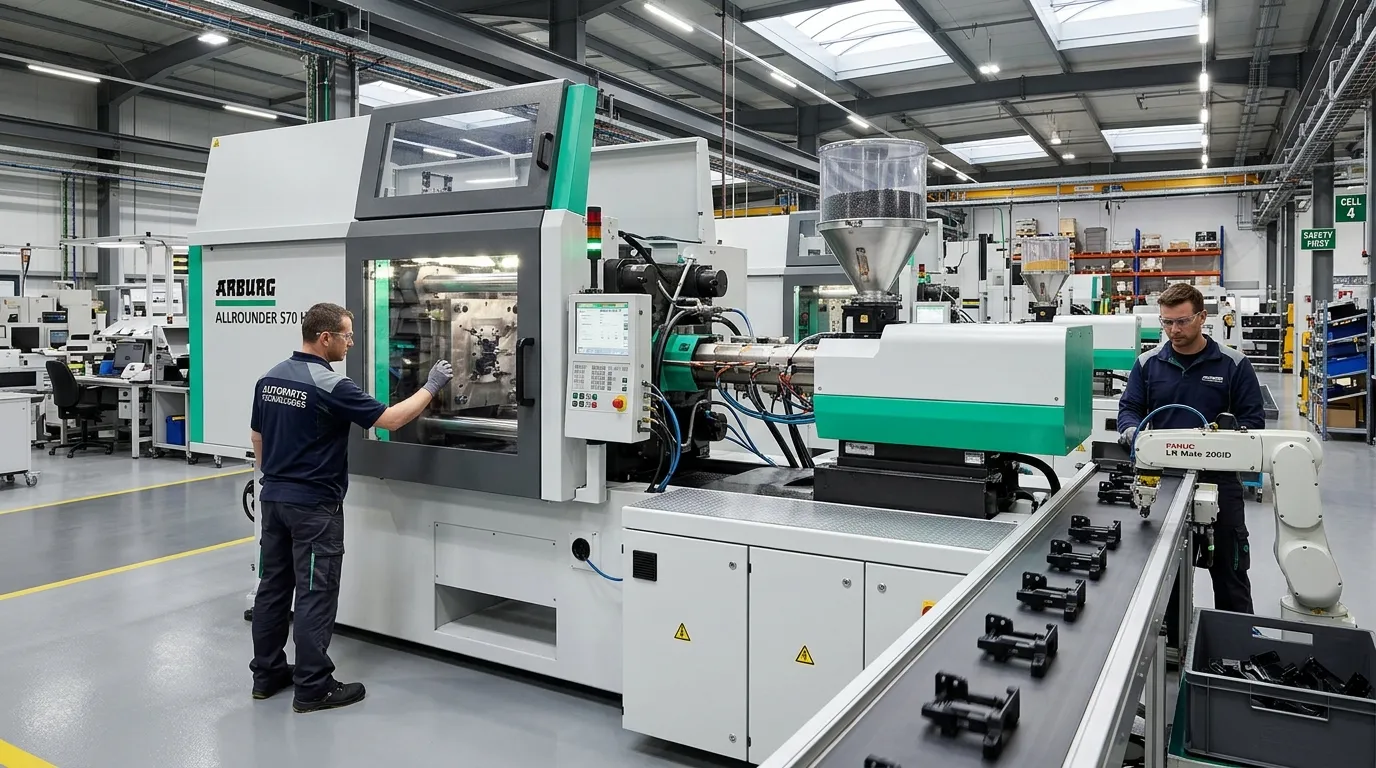
High-precision horizontal injection moulding engineered for consistent, high-volume production of complex plastic components across demanding automotive and home appliance sectors.
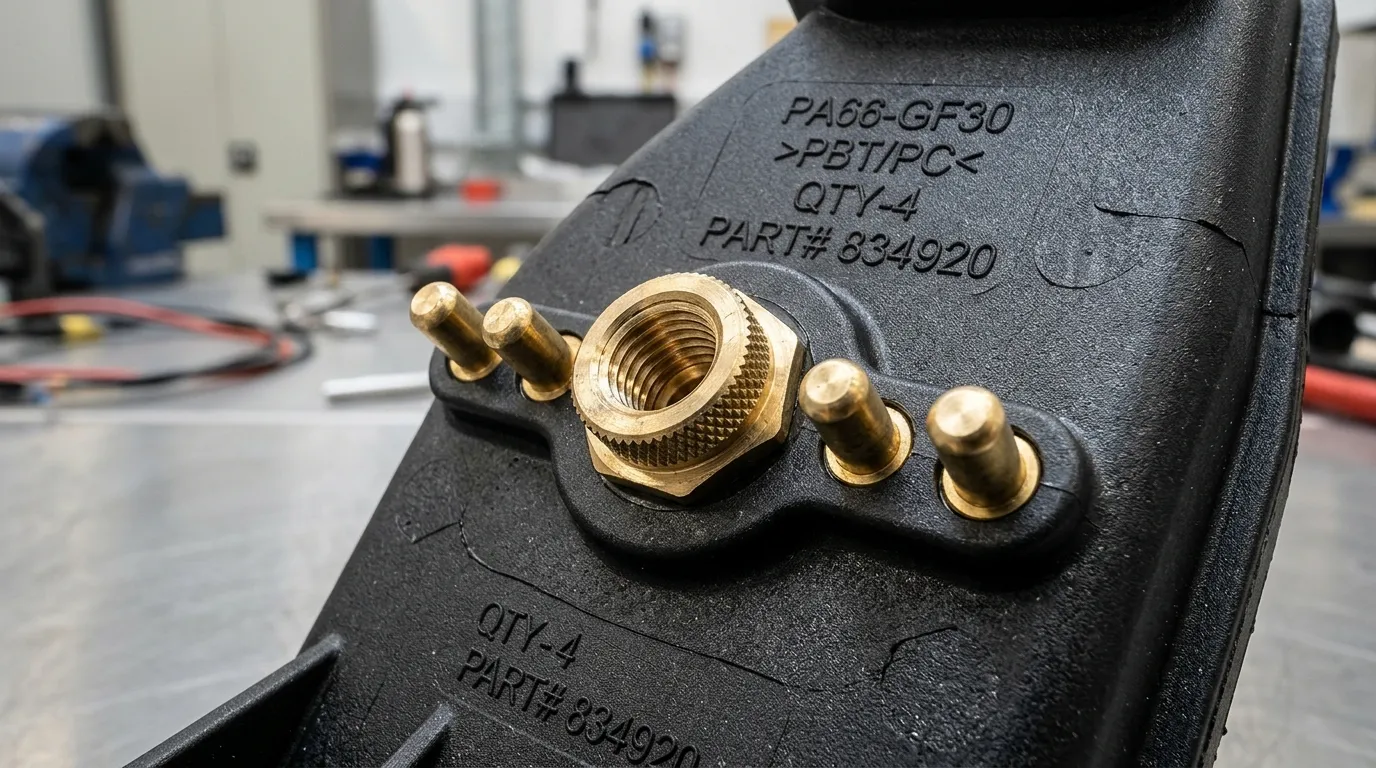
Seamlessly encapsulating metal fasteners, threaded bushings, and conductive terminals into high-grade engineering polymers for durable structural integrity.
Looking for a reliable manufacturing partner for your next component or assembly? Connect with our team to discuss your application, specifications, and production requirements.